T A B L E 2
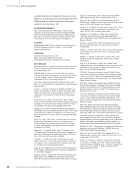
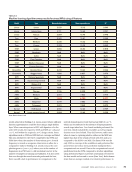
Capabilities and limitations of state-of-the-art NDE techniques for axle inspection
NDE methods Axle type Advantages Limitations
Fluorescent
MT (wet) Solid/hollow • Detects surface-breaking cracks
and subsurface cracks
• Requires removal of bearing components
and backing ring
• High operator dependence
• Hazardous waste generated
Automated
ACFM system Solid/hollow
• Large coverage of axle body
(requires array probe)
• Detects surface-breaking cracks
• Signals are electronically recorded
• Lacks the ability to inspect axles underneath the
wheel seats, bearings, and journal fillet areas
• Requires higher operator skill level
to interpret signals
ICFPD Solid/hollow • Detects fretting fatigue cracks
• Does not require removal of wheelsets
• Requires higher operator skill level
to interpret signals
• Limited to laboratory, not heavily
explored for field implementation,
so there are unknowns
Low-angle UT
scan Solid
• Detects internal cracks
• Can be carried out with limited access
and on axles in repair depots
• Apparent low sensitivity
Near-end/
high-angle UT
scan
Solid • Detects internal cracks
• Inspection can be done from axle end • Requires removal of bearing caps
Automated
UT system Solid/hollow • Detects internal cracks
• Fully automated UT system
• Requires removal of bearing components
and backing rings
• Requires higher operator skill level to
interpret signals
Automated
PAUT systems Solid/hollow
• Detects internal cracks
• Allows automated scanning of a larger surface area
• Inspection can be performed from either
the barrel or the end of an axle
• Requires removal of bearing/components
and backing rings
• Requires wheelsets to be dismounted
and bearing cap removed
AC
thermography Solid/hollow • Allows quick inspection
• Does not require coupling
• Can only inspect the barrel of the axle
• Lacks the ability to inspect axles underneath the
wheel seat, bearings, and journal fillet areas
• Deep defects like forging defects cannot be detected
• Generating AC field in axle is complicated for
in-motion inspection
Laser UT Solid
• Noncontact method and does not require
liquid couplant
• Allows quick inspection
• Technology is too sensitive to the extreme
operating environment of the railroad
• Can only inspect the barrel of the axle
• Design challenges were unable to be resolved
with the as-designed prototype
DIC Solid
• Whole-field strain measurement technique
• Noncontact method and does not
require liquid couplant
• Can only inspect the barrel of the axle
• Lacks the ability to inspect axles underneath the
wheel seat, bearings, and journal fillet areas
• Resolution was not sufficient to detect the stress
concentration due to a notch cut into the axle
• Implementation issues with surface preparation
and data acquisition under moving train
Laser
shearography Solid
• Whole-field NDE measurement technique
• Very sensitive to surface and subsurface
defects in axles
• Noncontact method, does not require couplant
• Can only inspect the barrel of the axle
• Lacks the ability to inspect axles underneath the
wheel seat, bearings, and journal fillet areas
• Deep defects like forging defects cannot be detected
• Implementation concerns for in-motion inspection
Resonance Solid/hollow • Detects shifts in the axle resonance frequencies
induced by cracks in the axle
• Baseline resonance readings need to be
stored for every axle
• Implementation concerns for in-motion inspection
Flash IRT Solid/hollow
• Noncontact method and does not require
liquid couplant
• Allows quick inspection
• Does not require coupling
• Can only inspect the barrel of the axle
• Lacks the ability to inspect axles underneath the
wheel seat, bearings, and journal fillet areas
• Deep defects like forging defects cannot be detected
• Requires large bank of capacitors and may pose
implementation concerns for in-motion inspection
FEATURE
|
RAILROADS
36
M A T E R I A L S E V A L U A T I O N • J A N U A R Y 2 0 2 4
2401 ME January.indd 36 12/20/23 8:01 AM
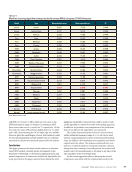
Capabilities and limitations of state-of-the-art NDE techniques for axle inspection
NDE methods Axle type Advantages Limitations
Fluorescent
MT (wet) Solid/hollow • Detects surface-breaking cracks
and subsurface cracks
• Requires removal of bearing components
and backing ring
• High operator dependence
• Hazardous waste generated
Automated
ACFM system Solid/hollow
• Large coverage of axle body
(requires array probe)
• Detects surface-breaking cracks
• Signals are electronically recorded
• Lacks the ability to inspect axles underneath the
wheel seats, bearings, and journal fillet areas
• Requires higher operator skill level
to interpret signals
ICFPD Solid/hollow • Detects fretting fatigue cracks
• Does not require removal of wheelsets
• Requires higher operator skill level
to interpret signals
• Limited to laboratory, not heavily
explored for field implementation,
so there are unknowns
Low-angle UT
scan Solid
• Detects internal cracks
• Can be carried out with limited access
and on axles in repair depots
• Apparent low sensitivity
Near-end/
high-angle UT
scan
Solid • Detects internal cracks
• Inspection can be done from axle end • Requires removal of bearing caps
Automated
UT system Solid/hollow • Detects internal cracks
• Fully automated UT system
• Requires removal of bearing components
and backing rings
• Requires higher operator skill level to
interpret signals
Automated
PAUT systems Solid/hollow
• Detects internal cracks
• Allows automated scanning of a larger surface area
• Inspection can be performed from either
the barrel or the end of an axle
• Requires removal of bearing/components
and backing rings
• Requires wheelsets to be dismounted
and bearing cap removed
AC
thermography Solid/hollow • Allows quick inspection
• Does not require coupling
• Can only inspect the barrel of the axle
• Lacks the ability to inspect axles underneath the
wheel seat, bearings, and journal fillet areas
• Deep defects like forging defects cannot be detected
• Generating AC field in axle is complicated for
in-motion inspection
Laser UT Solid
• Noncontact method and does not require
liquid couplant
• Allows quick inspection
• Technology is too sensitive to the extreme
operating environment of the railroad
• Can only inspect the barrel of the axle
• Design challenges were unable to be resolved
with the as-designed prototype
DIC Solid
• Whole-field strain measurement technique
• Noncontact method and does not
require liquid couplant
• Can only inspect the barrel of the axle
• Lacks the ability to inspect axles underneath the
wheel seat, bearings, and journal fillet areas
• Resolution was not sufficient to detect the stress
concentration due to a notch cut into the axle
• Implementation issues with surface preparation
and data acquisition under moving train
Laser
shearography Solid
• Whole-field NDE measurement technique
• Very sensitive to surface and subsurface
defects in axles
• Noncontact method, does not require couplant
• Can only inspect the barrel of the axle
• Lacks the ability to inspect axles underneath the
wheel seat, bearings, and journal fillet areas
• Deep defects like forging defects cannot be detected
• Implementation concerns for in-motion inspection
Resonance Solid/hollow • Detects shifts in the axle resonance frequencies
induced by cracks in the axle
• Baseline resonance readings need to be
stored for every axle
• Implementation concerns for in-motion inspection
Flash IRT Solid/hollow
• Noncontact method and does not require
liquid couplant
• Allows quick inspection
• Does not require coupling
• Can only inspect the barrel of the axle
• Lacks the ability to inspect axles underneath the
wheel seat, bearings, and journal fillet areas
• Deep defects like forging defects cannot be detected
• Requires large bank of capacitors and may pose
implementation concerns for in-motion inspection
FEATURE
|
RAILROADS
36
M A T E R I A L S E V A L U A T I O N • J A N U A R Y 2 0 2 4
2401 ME January.indd 36 12/20/23 8:01 AM